Size the usable surface, not the room
The first number is the largest workpiece footprint in its welding position. The table must support the locating points and clamping points, not necessarily every millimetre of the part. A frame may overhang safely when its supported datums remain on the table and the overhang does not create an unstable load; a small assembly may need more table area than its footprint because clamps approach from outside the part.
Sketch the workpiece on a rectangle and mark every clamp, stop, angle square and access path. Add clearance only where a tool or operator actually needs it. This produces a useful working envelope instead of an oversized table that increases reach and floor-space requirements.
- Mark the largest and smallest workpiece footprint handled at the station.
- Add the width of clamps and stops outside each datum edge.
- Keep weld seams, tack points and inspection features reachable after clamping.
- Show any intentional overhang and how the projecting weight will be supported.
Use a simple working-height calculation
The table top is only one layer in the working height. The operator works at the weld or assembly feature, which may sit above a support block, fixture plate and the workpiece itself. Measure the operator elbow height in the normal footwear and posture used at the station, then subtract the stack between the tabletop and the working feature.
Working height = operator elbow height - fixture stack - workpiece height to the working feature. Treat the result as a starting point and test it with the real process. Precision fitting often benefits from a higher working feature for visibility, while forceful clamping and handling generally need more room to work above the part.
| Input | Measure from | Why it matters |
|---|---|---|
| Operator elbow height | Floor to elbow in the normal working posture | Sets the reference for comfortable reach |
| Fixture stack | Tabletop to the part datum | Raises the whole workpiece above the table |
| Workpiece height | Part datum to the main working feature | Places the actual weld or assembly point |
| Handling allowance | Crane hook, trolley, fork or positioner path | Prevents the chosen height from blocking material flow |
Check reach before adding table width
A wider table creates more fixture space but also moves the centre farther from the operator. Before choosing the largest available platform, decide whether the job can be approached from both long sides and whether the table can be moved away from a wall. Side-face clamping can reduce the need to reach across the top because stops and supports can attach to the vertical faces.
For long frames, length is often more useful than width. For compact assemblies surrounded by tooling, extra width may be necessary even when the part itself is narrow. The correct proportion follows the clamp plan rather than a standard workshop ratio.
Match the platform body and support
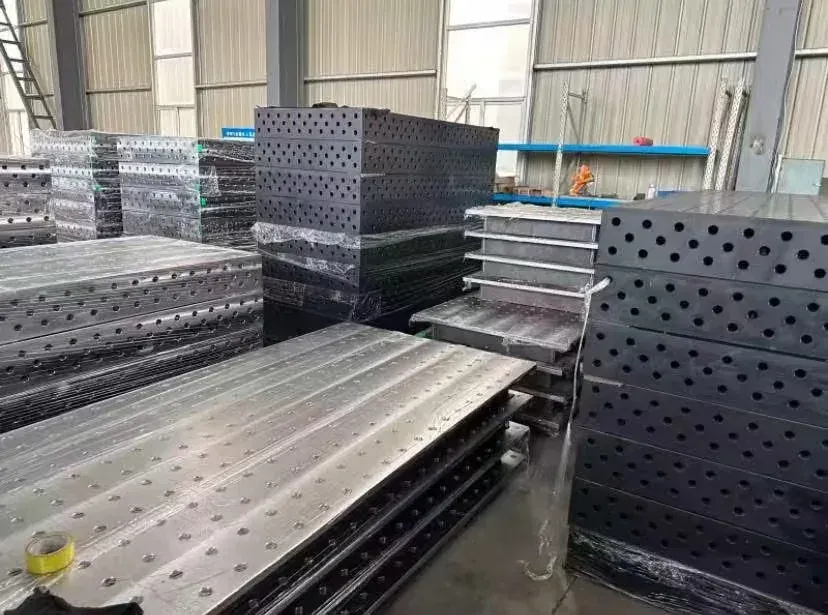
BECO platforms are available from 500 x 500 mm to 4000 x 2000 mm. Platform body heights are 100 or 200 mm, with custom heights available. The body height is not the same as the final working height: legs, cabinets, levelling feet, mobile bases and the fixture stack all contribute to the finished station.
Confirm whether the table will stay in one levelled position, move between cells or interface with another machine. A mobile base changes stability and working height; a fixed support allows the station to be levelled around one process. These choices should be shown on the quotation drawing rather than left until installation.
Choose the hole system after the envelope
Table dimensions and hole system solve different problems. Size determines whether the work and tooling fit; D16, D22 or D28 determines the spacing and scale of the compatible pins, clamps and stops. A large table can still use D16 for detailed fixtures, and a compact table may use D28 when the work is heavy. Decide from the workpiece and clamping load, not from the platform dimensions alone.
- D16: compact parts, fine positioning and close clamp placement.
- D22: mixed fabrication where one station covers several job sizes.
- D28: large frames, thick plate and higher clamping loads.
Send these dimensions with the RFQ
- Largest workpiece length, width, height and weight in its welding position.
- Smallest recurring part and any shared datum used across the product family.
- A marked-up drawing showing clamp access, overhang and side-face use.
- Operator posture: standing, seated, shared station or robot-loaded.
- Fixture and support stack above the tabletop.
- Material-handling method and any required interface height.
- Preferred D16, D22 or D28 system, or the clamping load for recommendation.